Our Manufacturing

BUILT WITH PRECISION.
MADE PRIME.

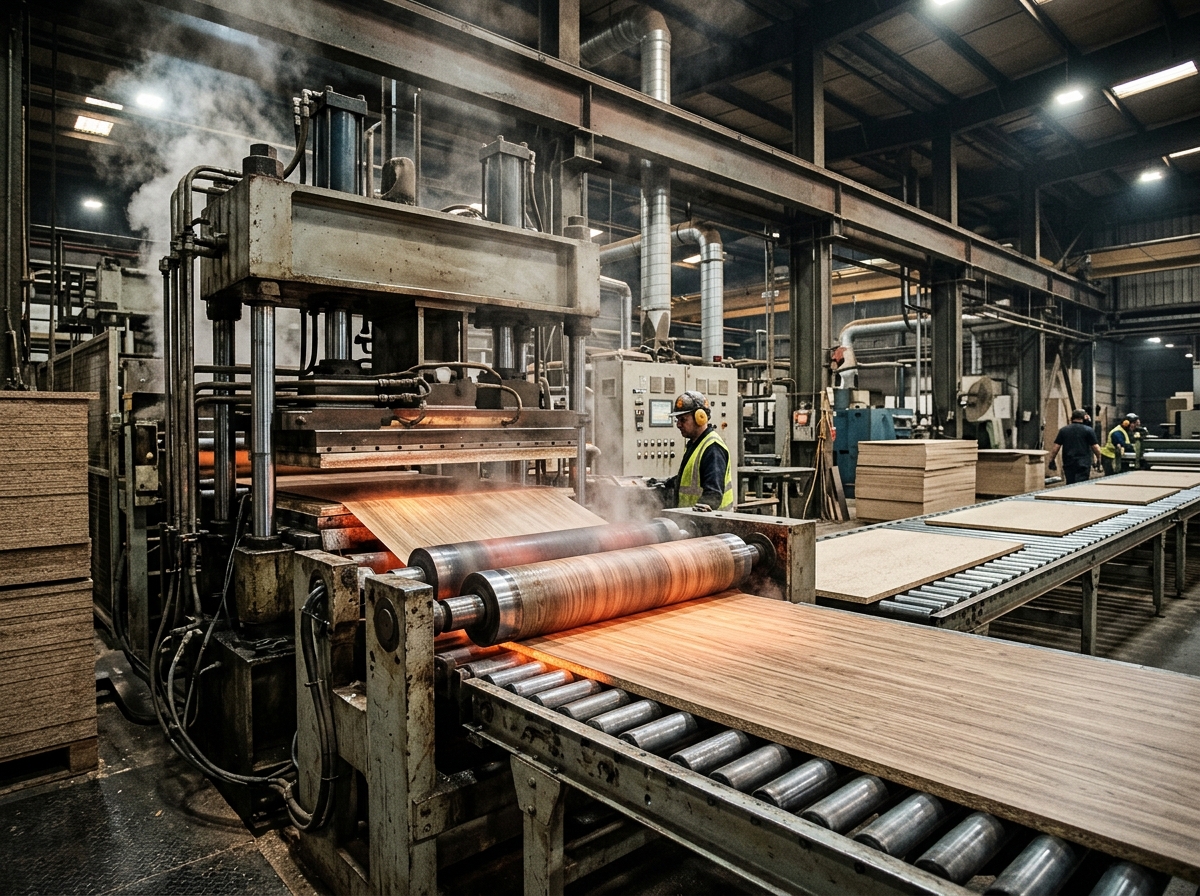
From sugarcane bagasse to BIS-certified engineered boards — our state-of-the-art manufacturing facility combines German press technology with two decades of Indian craftsmanship.

0+

BOARDS / YEAR

0+

DEALERS

0+

YEARS LEGACY

Call Us Now

+91 98765 43210

Built With Precision.
Made Prime.

From sugarcane bagasse to BIS-certified engineered boards.
Advanced German technology, backed by two decades of Indian craftsmanship.

Production Process

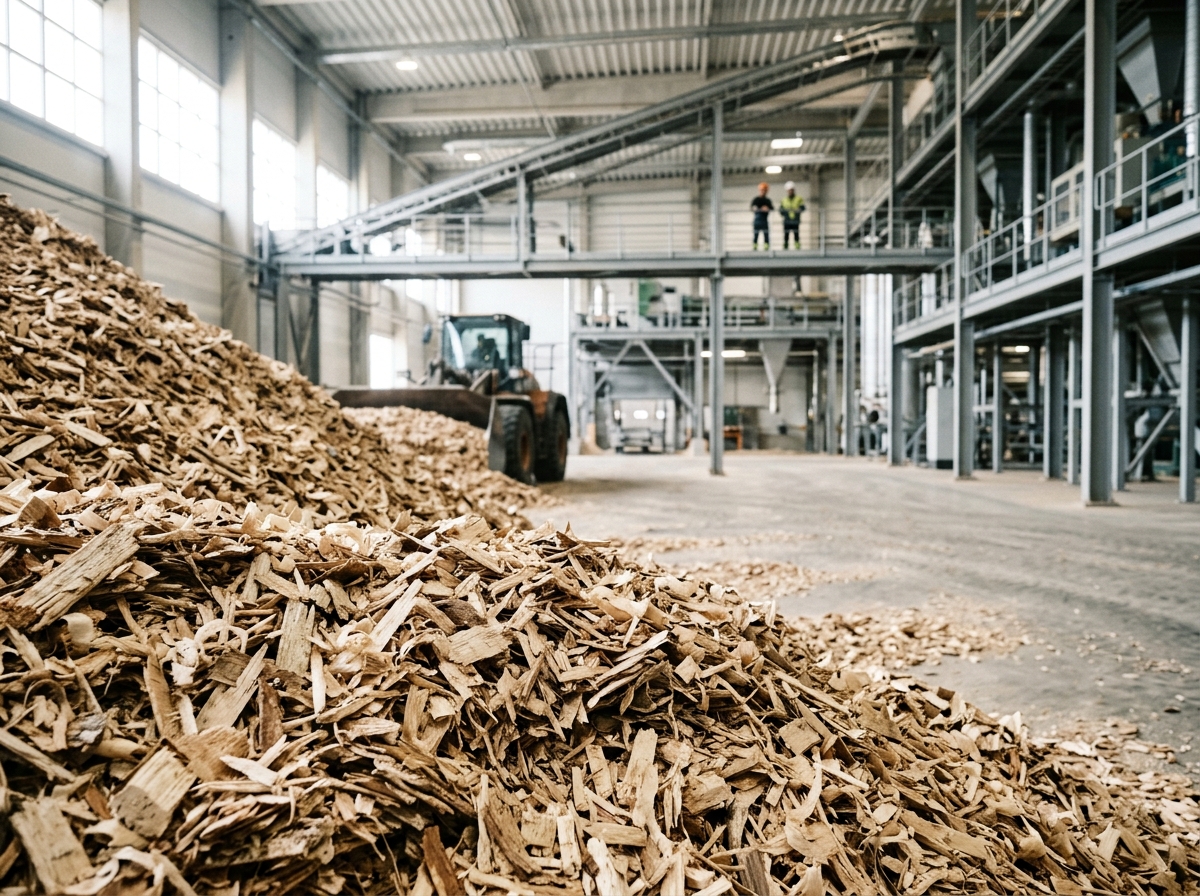
Step 1: High-Density Core Preparation

We source premium wood fibers, purify them, and mix them with eco-friendly adhesives. Pressed under high temperature, we form our signature HDF board with uniform density and ultimate load-bearing strength.

Step 2: Functional Layering

We carefully align the 4 core elements: High-purity Al₂O₃ wear paper (AC3-AC5), 1:1 HD digital decor paper (fade-resistant), the HDF core, and the bottom moisture-proof balance paper.—to engineer commercial waterproof laminate flooring that withstands heavy foot traffic and moisture exposure.

Step 3: 1400T Lamination

The 4-layer stack enters our fully automatic 2500-ton short-cycle pressing lines. Under extreme heat and pressure, the layers fuse permanently into a single solid blank, guaranteeing zero hollowing or delamination.

Step 1: High-Density Core Preparation

We source premium wood fibers, purify them, and mix them with eco-friendly adhesives. Pressed under high temperature, we form our signature HDF board with uniform density and ultimate load-bearing strength.

Step 1: High-Density Core Preparation

We source premium wood fibers, purify them, and mix them with eco-friendly adhesives. Pressed under high temperature, we form our signature HDF board with uniform density and ultimate load-bearing strength.

Step 1: High-Density Core Preparation

We source premium wood fibers, purify them, and mix them with eco-friendly adhesives. Pressed under high temperature, we form our signature HDF board with uniform density and ultimate load-bearing strength.

Our Manufacturing

BUILT WITH PRECISION.
MADE PRIME.

From sugarcane bagasse to BIS-certified engineered boards — our state-of-the-art manufacturing facility combines German press technology with two decades of Indian craftsmanship.

0+

BOARDS / YEAR

0+

DEALERS

0+

YEARS LEGACY
Our Manufacturing

Built With Precision.
Made Prime.

From sugarcane bagasse to BIS-certified engineered boards — our state-of-the-art manufacturing facility combines German press technology with two decades of Indian craftsmanship.

0+

BOARDS / YEAR

0+

DEALERS

0+

YEARS LEGACY
Our Manufacturing

BUILT WITH PRECISION.
MADE PRIME.

From sugarcane bagasse to BIS-certified engineered boards — our state-of-the-art manufacturing facility combines German press technology with two decades of Indian craftsmanship.

0+

BOARDS / YEAR

0+

DEALERS

0+

YEARS LEGACY
Inside the Plant

See The Machines Behind Every Boards

Our manufacturing unit spans a purpose-built facility equipped with continuous hot-press lines, precision CNC saws, and an air-controlled QC laboratory — all operating under one roof for end-to-end accountability.

Every process is carefully controlled for superior quality.

Production Process

01.

Row Material

We source premium wood fibers, purify them, and mix them with eco-friendly adhesives. Pressed under high temperature, we form our signature HDF board with uniform density and ultimate load-bearing strength.

02.

Forming

We carefully align the 4 core elements: High-purity Al₂O₃ wear paper (AC3-AC5), 1:1 HD digital decor paper (fade-resistant), the HDF core, and the bottom moisture-proof balance paper.—to engineer commercial waterproof laminate flooring that withstands heavy foot traffic and moisture exposure.
03.

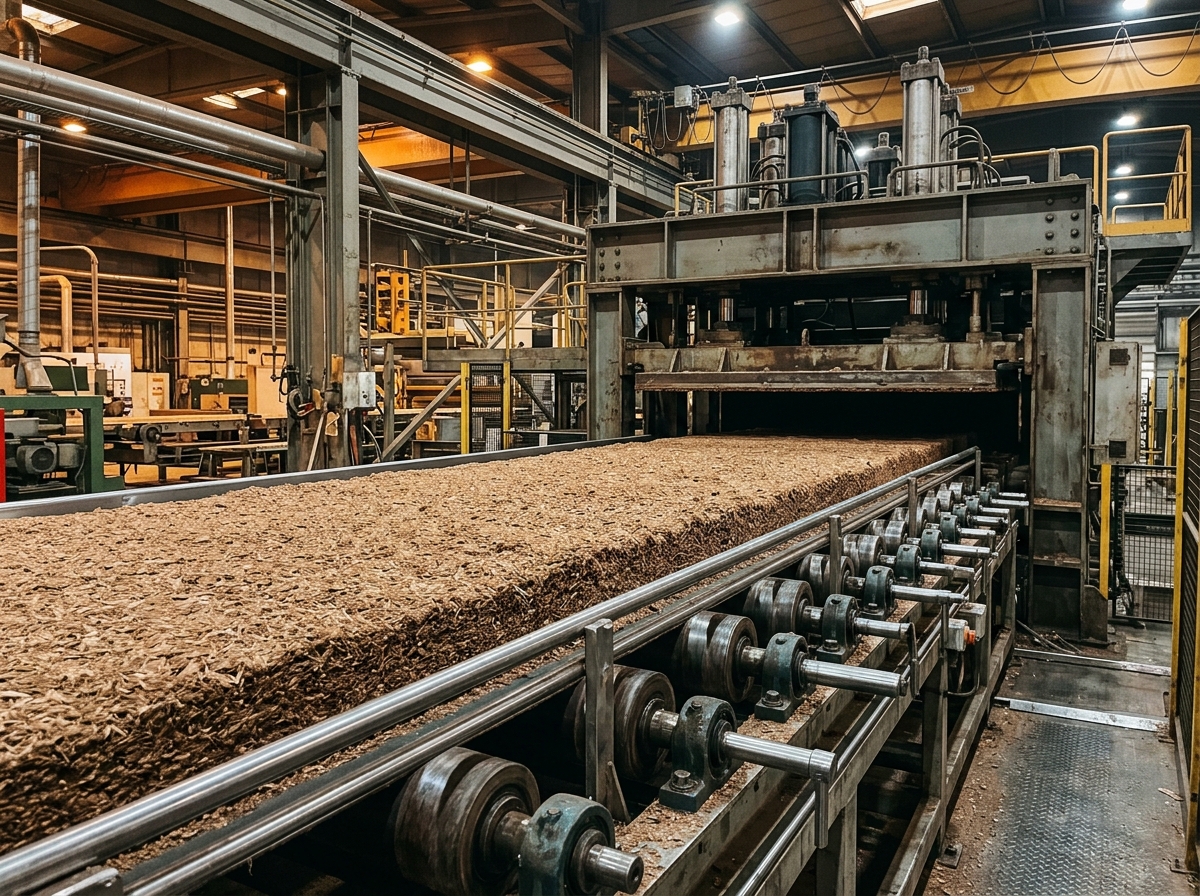
Pressing

The 4-layer stack enters our fully automatic 2500-ton short-cycle pressing lines. Under extreme heat and pressure, the layers fuse permanently into a single solid blank, guaranteeing zero hollowing or delamination.

04.

Lemination

The hot blanks travel through an automated cooling line to stabilize the internal structure and prevent future warping—ensuring every plank of our commercial waterproof laminate flooring retains its shape under heavy use. Then, CNC equipment slices them into precise dimensions with razor-sharp edges.

05.

Quality Check

Qualified planks are securely packed using moisture-proof and anti-collision materials. Clear, accurate labeling (specs, AC rating, eco-grade) ensures the commercial waterproof laminate flooring product is ready for global distribution.